Repair & life extension
HIP is a metallurgical reset, not a cosmetic polish. Operators ask whether a set of first-stage blades can run another interval instead of going to scrap. The answer is written in remaining wall, crack limits and alloy recipe — not in a brochure promise.
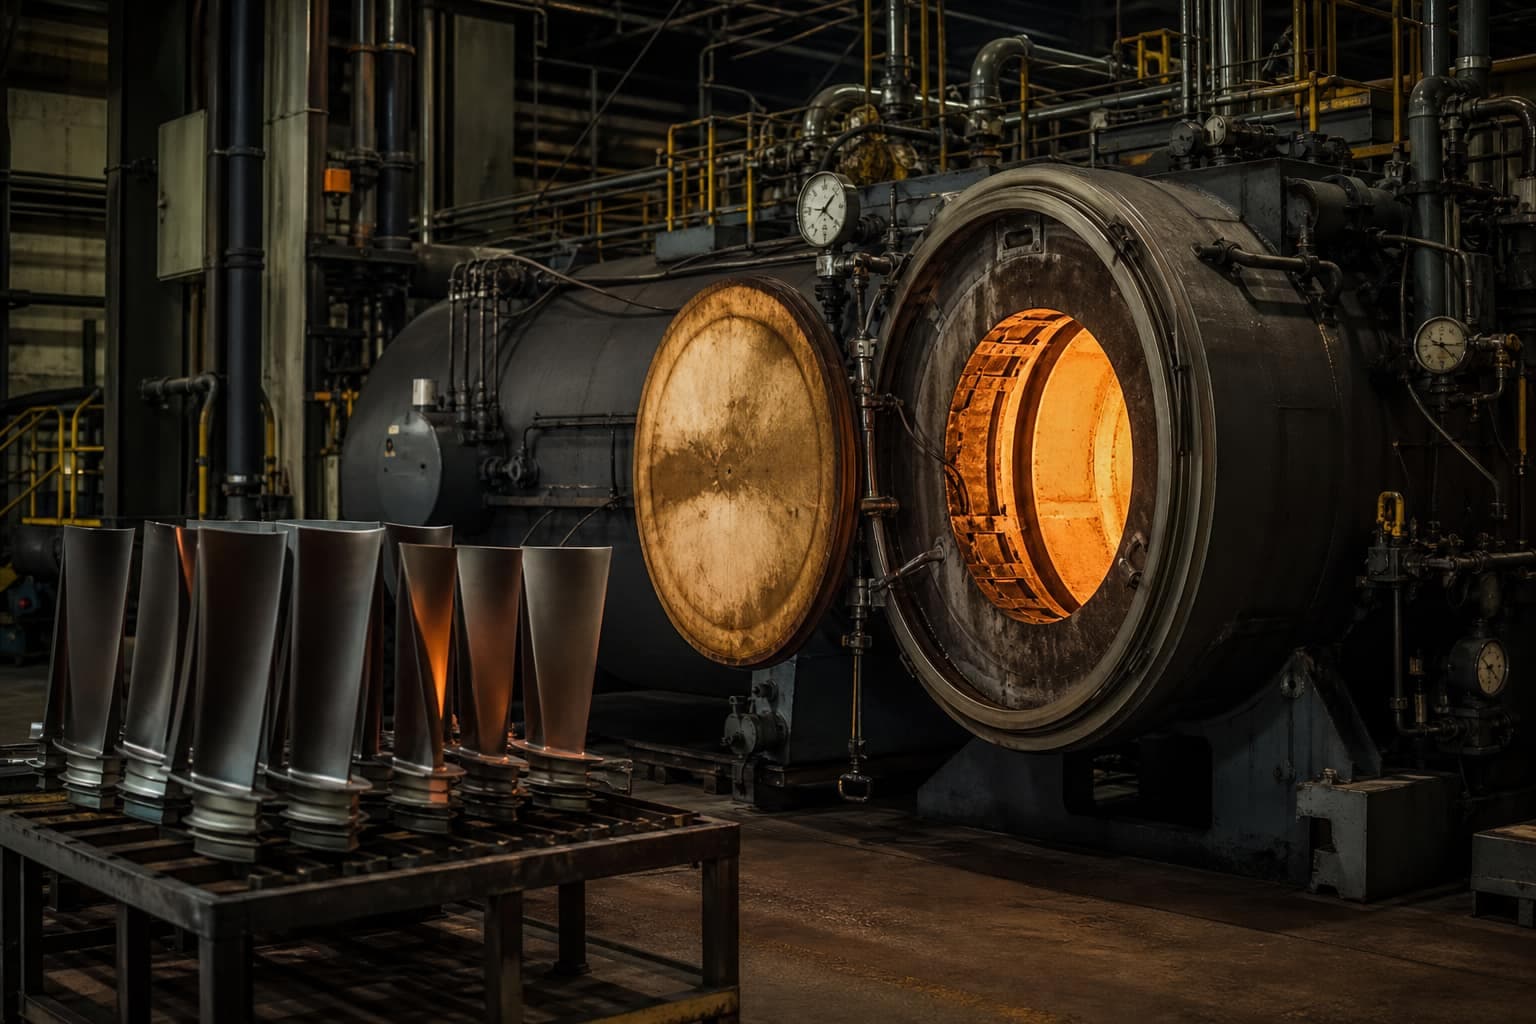
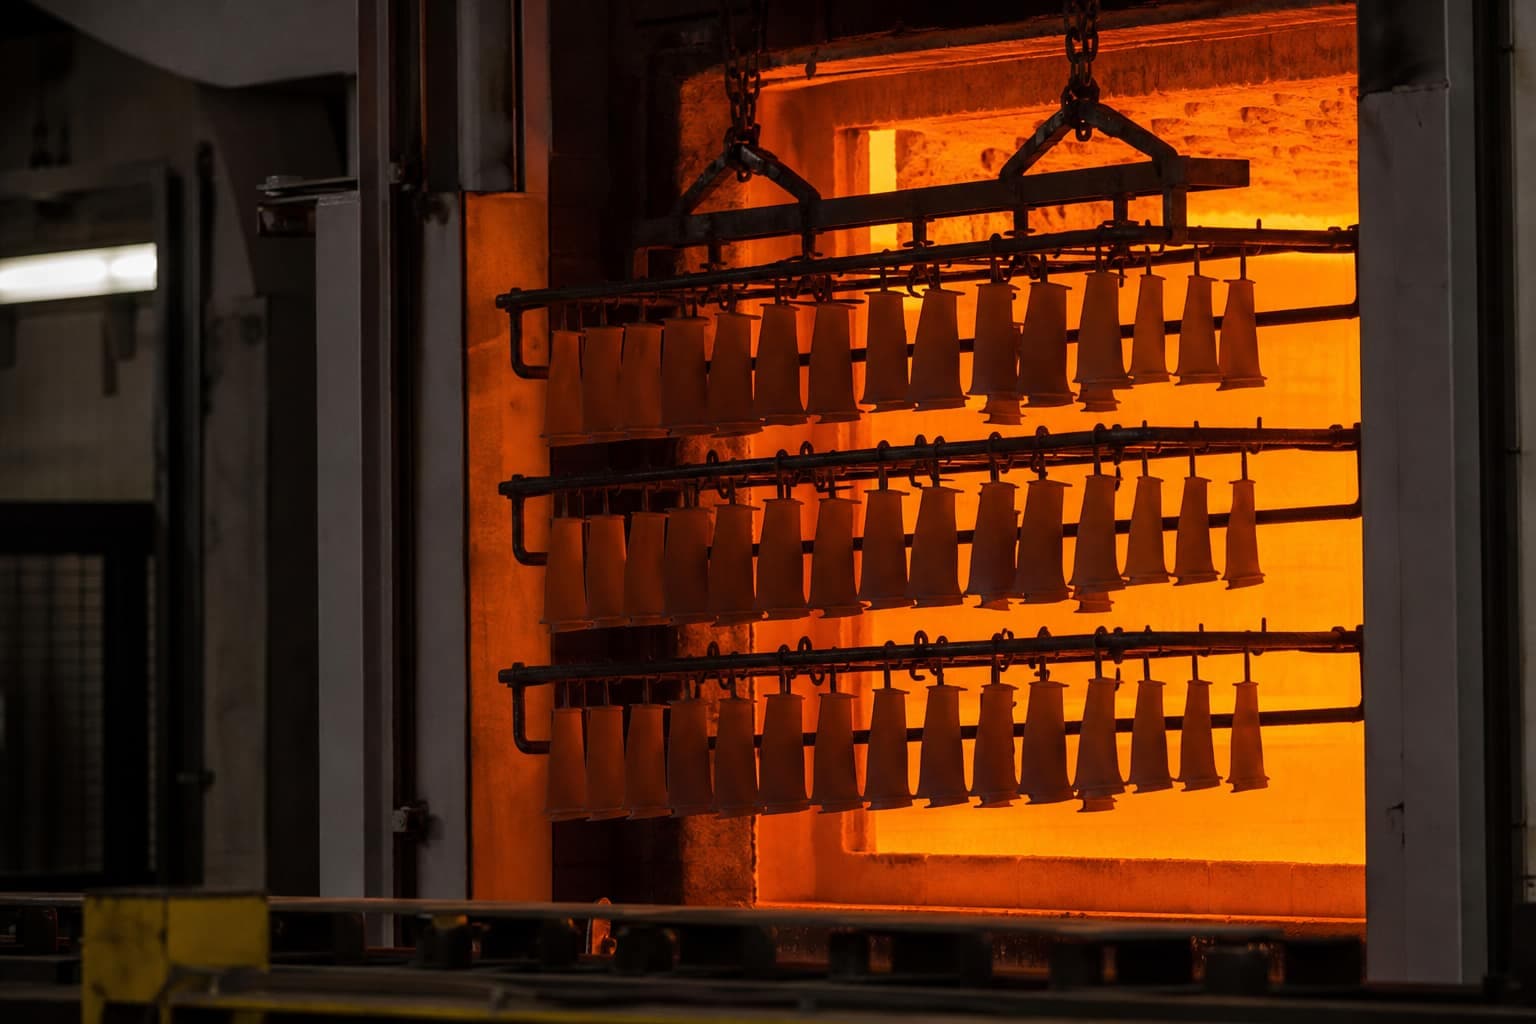
HIP is hot isostatic pressing: blades sit in a sealed vessel, are heated, and are pressed with inert gas until internal voids close and the creep-damaged microstructure recovers toward a near-new condition. Typical cycles sit around 1200 °C and 100–200 MPa. HIP does not grow missing airfoil metal. That is weld or new-make. After the vessel, Euroturbine strips and reapplies TBC or MCrAlY — thermal barrier coating or the metallic bond layer — as specified, and releases the set only after NDT. NDT means non-destructive testing. Typical yield on suitable alloys has been around 90 percent in our repair history. The gate is still remaining wall and crack limits, not a brochure percentage.
Result 1 — HIP plus recoat
This is the job when NDT or metallography shows internal voids, remaining wall is still inside the repair minimum, cracks are absent or inside blend limits, and the alloy is a HIP candidate — typically equiax or directionally solidified nickel such as MM247, GTD111, Rene 80 or IN738 class. Incoming inspection maps FPI indications, wall thickness and previous repairs. Coating is stripped so the vessel sees the substrate. After HIP the blade is still coated and inspected. HIP alone without a full recoat is not a complete rejuvenation. The surface still needs the environmental and thermal barrier that row was designed with.
Case. A combined-cycle 9E first-stage bucket. X-ray shows internal voids. Remaining wall is still inside limit. The leading-edge coating is tired, the metal underneath is sound, cooling holes are open. Euroturbine writes HIP plus recoat, not new-make. The commercial is a fraction of a new bucket. The engineering is remaining wall and a known HIP recipe — not a hope that pressure will grow metal. Single-crystal rows need a separate review. Do not paste an equiax HIP recipe onto SX.
Result 2 — Blend or allowed weld, no HIP
This is the job when the indication is local, remaining wall is enough, and there are no internal voids that need a vessel. A tip rub, a small trailing-edge nick, a blendable leading-edge ding. Euroturbine writes blend or an allowed weld, heat treatment, then recoat if the row is coated. HIP is not a cheaper weld. Booking the vessel because “بازسازی” sounds more complete is how you spend money on a sound casting.
Case. A V94.2 first-stage vane with a local tip rub and a clean X-ray. Wall map is inside limit. No porosity cluster. Euroturbine writes blend, heat treat, recoat. The vessel stays empty for that serial. If the next vane in the same crate shows a void map, that serial can still go to result 1. The decision is per piece, not one adjective for the crate.
Result 3 — Replace the set
This is the job when airfoil metal is gone, trailing-edge burn-through is outside the repair spec, a crack has entered the root, cooling will not pass airflow, or repeated HIP and weld cycles have already used the alloy budget. HIP does not rebuild a hole. A geometry or cooling upgrade the frame now needs also cannot be restored from a worn serial. Euroturbine writes scrap for that piece and new-make for the OEM number.
Case. An SGT-600 power-turbine blade with trailing-edge burn-through and wall below the minimum. The station asks whether HIP can “save” it because a sister set is already in the vessel. Euroturbine writes replace. Mixing that serial back into a HIP batch would hide result 3 under a ceramic. If only part of a 9E set is scrap, the honest plan is HIP the sound serials and new-make the rest, with mass and coating family signed before the row closes.
HIP plus recoat often lands at a fraction of new-blade cost — but only after remaining wall says the set still has a life case.
Send blade history, equivalent hours and starts, and the last NDT report — FPI, X-ray or wall map, whichever you have. If remaining life is unclear, remaining-life assessment (RLTA) belongs before the vessel is booked. Euroturbine will say result 1, 2 or 3 in writing, then quote. Do not book the vessel on a photograph.
Frequently asked questions
What does HIP actually do to a service-run blade?
High temperature (around 1200 °C) and inert-gas pressure (typically 100–200 MPa) close internal micro-voids and recover a more uniform microstructure after creep. It does not rebuild missing airfoil metal; that is weld repair.
Which alloys respond well?
Euroturbine’s rejuvenation route is proven on MM247, GTD111 and Rene 80 when remaining wall thickness and crack limits allow. Single-crystal blades need a separate engineering review.
Should RLTA come before HIP?
Yes when operating hours, previous repairs or coating condition are unclear. Remaining life assessment tells you whether HIP plus recoat is justified or whether the set should be replaced.
Related reading
Have a blade set waiting on a HIP decision?
Euroturbine agrees repair limits in writing before the vessel cycle and can mix HIP with new-make blades if only part of the set is scrap.
Talk to repair engineeringMore articles
Buying Hot-Gas-Path Parts for the GE MS6001B Frame 6B
IN738, IN738LC and IN939 Turbine Blades: What the Alloy Grade Specifies
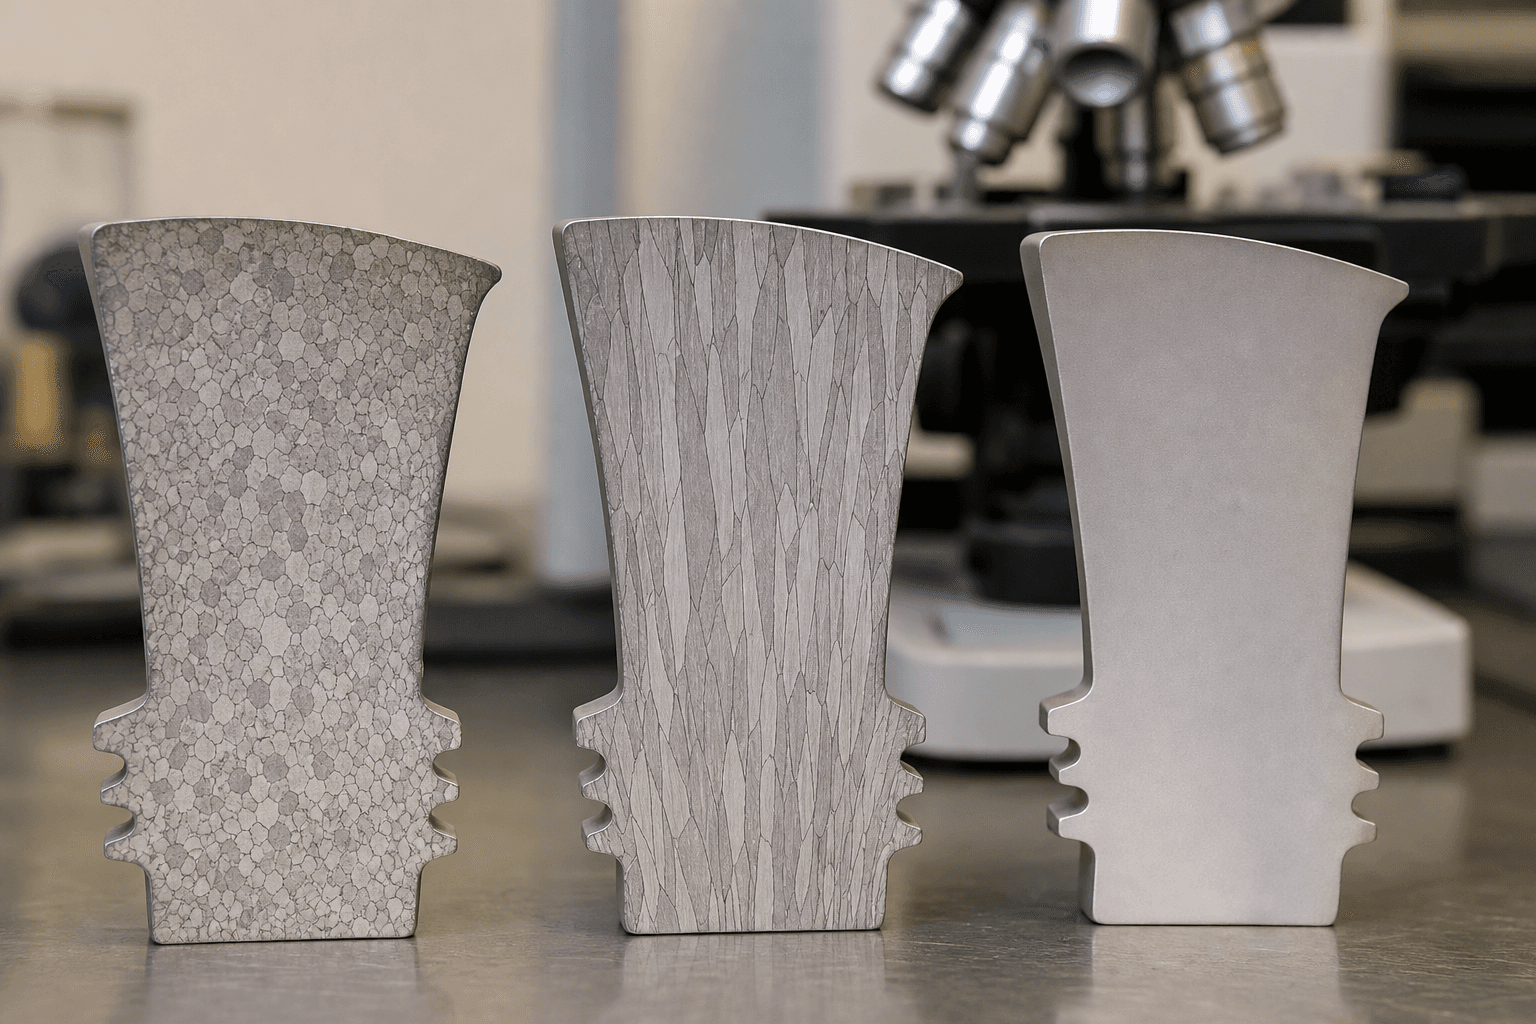
Equiaxed, Directionally Solidified and Single-Crystal Blades: Three Different Products
Fir-Tree Blade Roots and Turbine Discs: The Blade Is Cast, the Disc Is Forged

Aftermarket Parts for a Siemens SGT-400 Oil-and-Gas Package
Last updated: August 29, 2026